


How to Audit IP65 Stage Light Quality Before Factory Shipment
- Pre-Shipment Quality Framework for Weather-Resistant Stage Lighting
- Define the acceptance criteria before production
- Check the meaning and evidence behind the enclosure rating
- Audit documentation and traceability
- Physical, Electrical, and Optical Inspection at the Factory
- Inspect the enclosure, seals, and cable-entry system
- Verify electrical safety and operating stability
- Measure light output and thermal performance
- Sampling, Burn-In, and Independent Factory Verification
- Use a risk-based sampling plan
- Run controlled aging and environmental checks
- Invite third-party inspection when project risk is high
- Why Colorful Light Supports a More Controlled Procurement Process
- Manufacturing and quality-control capability
- Product coverage for professional applications
- Compliance, warranty, and long-term value
- Final Release Checklist for Buyers
- Documents to approve
- Physical checks to complete
- Commercial release decision
- Frequently Asked Questions
A reliable pre-shipment audit for an IP65 Stage Light should verify more than a product label. Buyers need evidence that the enclosure, cable glands, connectors, cooling architecture, LED engine, control system, and mechanical assemblies can perform consistently in outdoor events, touring productions, festivals, architectural entertainment venues, and other demanding applications. The audit should combine document review, production-line inspection, sample testing, functional burn-in, sealing verification, and final packing checks. The IEC explanation of IP ratings identifies the first digit as protection against solid objects and the second digit as protection against water; therefore, an IP65 claim must be evaluated as a defined protection level rather than treated as a general promise of weatherproof performance.
Pre-Shipment Quality Framework for Weather-Resistant Stage Lighting
Define the acceptance criteria before production
The purchase order should state the required ingress protection rating, operating environment, rated voltage, frequency, LED power, color temperature or color range, dimming behavior, control protocol, fixture dimensions, weight, mounting method, and warranty terms. It should also identify whether the equipment will be installed under temporary outdoor structures, exposed to direct rain, transported frequently, or operated near coastal air. These conditions influence the appropriate enclosure materials, fasteners, coatings, connectors, drainage strategy, and maintenance plan.
Buyers should request the approved product specification, bill of materials, wiring diagram, user manual, risk assessment, inspection plan, and sample approval record. A supplier that cannot connect the shipped unit to a controlled specification creates avoidable disputes over brightness, beam angle, noise, color consistency, and environmental performance. Acceptance criteria are particularly important for strobe lights, blinder lights, wash lights, par can lights, and moving head fixtures because similar product names can conceal substantial differences in LED configuration and optical output.
Check the meaning and evidence behind the enclosure rating
For the IP code, the number six indicates dust-tight protection under the applicable test conditions, while the number five indicates protection against water jets from defined directions and test parameters. This does not automatically mean the fixture is suitable for permanent immersion, high-pressure cleaning, salt spray, condensation inside a cold enclosure, or unrestricted exposure to extreme weather. The ISO 9001 quality management standard provides a useful framework for evaluating whether inspection activities are controlled and traceable, but ISO 9001 certification alone is not proof that a particular luminaire passed an ingress test.
Ask for the test method, test date, tested configuration, sample identification, laboratory or internal test facility, and result. The report should correspond to the exact housing, gasket design, cable entry, connector arrangement, and glass or lens assembly used in the shipment. A report for an earlier revision or a visually similar housing should not be accepted as equivalent without technical justification.
Audit documentation and traceability
Every production batch should have a lot number or serial-number range linked to incoming-material inspection, assembly records, electrical tests, aging results, and final inspection. Traceability enables a distributor or project owner to isolate affected units if a driver, gasket, fan, connector, or control board later shows a recurring defect. It also helps the manufacturer identify whether a failure originated in a purchased component, assembly process, software version, or transport event.
Compliance documentation should be reviewed carefully. The European Commission CE marking guidance explains that CE marking represents a manufacturer’s declaration that applicable EU requirements have been met; it is not a universal performance certificate and does not replace product-specific testing. Similarly, the European Commission RoHS information concerns restriction of certain hazardous substances in electrical and electronic equipment. Buyers should check that declarations, technical files, labels, and supplied models are consistent.
Physical, Electrical, and Optical Inspection at the Factory
Inspect the enclosure, seals, and cable-entry system
Begin with a visual and dimensional inspection of the housing. Look for casting porosity, sharp edges, incomplete coatings, corrosion marks, loose screws, cracked lenses, warped panels, and inconsistent joints. Verify that the rear cover closes evenly and that compression gaskets sit continuously in their grooves rather than being pinched, stretched, contaminated, or interrupted at corners. Fasteners should be tightened according to a controlled procedure; excessive torque can deform a seal, while insufficient torque can create a leakage path.
Cable glands and connectors deserve special attention because they are common weak points. Confirm that the cable diameter matches the gland range, the strain relief is secure, unused entries are properly sealed, and connectors are fully locked. Check whether external connectors are genuinely rated for the intended environment and whether protective caps are supplied for transport and installation. Inspect drain or pressure-equalization features where used, ensuring that membranes are not blocked by paint, adhesive, dust, or assembly debris.
Verify electrical safety and operating stability
Factory inspection should include grounding continuity, insulation resistance, dielectric withstand where specified, leakage current, polarity, connector pinout, input-current behavior, and protection against abnormal operating conditions. The exact test limits should come from the product design and applicable safety standards rather than an arbitrary internal value. A qualified electrical technician should operate the equipment through its permitted voltage range and confirm that the power supply, LED driver, control board, display, cooling system, and protection circuits behave correctly.
Functional testing should cover DMX control, RDM functions when offered, standalone programs, dimming from low to full output, strobe frequency, color mixing, macros, reset behavior, loss and restoration of signal, and fixture addressing. For automated luminaires, pan and tilt movement should be checked for abnormal noise, backlash, cable drag, end-stop errors, and calibration drift. Testing only at full white output can miss problems in low-level dimming, color transitions, shutter timing, or control-channel mapping.
Measure light output and thermal performance
Optical acceptance should compare production samples with the approved reference unit. Depending on the product, relevant measurements include illuminance, luminous flux, beam angle, color temperature, color rendering, chromaticity consistency, dimming linearity, and flicker characteristics. For a strobe or blinder, pulse uniformity and thermal behavior may matter more than beam precision. For a moving head wash or LED moving head, output consistency across pan and tilt positions, zoom range, color mixing, and lens cleanliness should be assessed.
Thermal testing should run the fixture long enough to reach a stable operating condition. Record housing temperature, LED-board temperature where accessible, driver temperature, fan speed, ambient temperature, and any thermal-protection response. A sealed enclosure cannot be evaluated only by its water resistance; heat accumulation can shorten LED, driver, capacitor, and display life. The IEC standards resources can help buyers identify the terminology and standard references that should appear in a supplier’s technical documentation, while the manufacturer remains responsible for applying the relevant product standards to the specific design.
| Audit area | Recommended evidence | Typical release decision |
|---|---|---|
| Enclosure protection | Model-specific ingress test record, visual seal inspection, connector review | Release only when the tested configuration matches the shipment |
| Electrical safety | Grounding, insulation, dielectric or leakage test records | Reject units with failed or missing safety results |
| Optical output | Photometric comparison against an approved sample | Investigate output or color deviation beyond agreed tolerance |
| Thermal stability | Full-load burn-in data and temperature records | Hold units showing overheating, abnormal noise, or protection trips |
| Control functions | DMX/RDM, dimmer, strobe, movement, and reset checklist | Release after all specified modes operate correctly |
| Packaging | Drop or vibration plan where applicable, carton and accessory checklist | Correct damage risks before container loading |
Sampling, Burn-In, and Independent Factory Verification
Use a risk-based sampling plan
Sampling should be agreed before the inspection date. AQL-based sampling can support visual and dimensional checks, but critical safety or ingress-related characteristics may require 100% verification or a dedicated test on representative samples. The ISO 2859-1 sampling standard is commonly referenced for attribute inspection, yet buyers should not apply a generic sampling level without considering product value, failure consequences, production maturity, and project scale.
For a mixed shipment containing strobe lights, city color lights, retro lights, follow spot lights, laser lights, and moving fixtures, samples should represent each model, revision, and production lot. Select units randomly from finished cartons rather than allowing only specially prepared demonstration samples. Record serial numbers and photograph the condition before testing so that the inspection result remains auditable.
Run controlled aging and environmental checks
A burn-in cycle exposes early failures in LED drivers, solder joints, fans, motors, power connectors, displays, and control boards. Operate sampled units through realistic scenes rather than leaving them at a single static setting. Include high-output white, saturated colors, dimming transitions, strobe operation, movement patterns, and signal interruption where relevant. Monitor restarts, flicker, error codes, fan changes, thermal alarms, and communication loss.
Water testing must follow a controlled procedure and should be performed by trained personnel. Confirm nozzle type, flow, pressure, distance, duration, fixture orientation, drain-down time, and post-test inspection method. After testing, inspect internal areas for droplets, fogging, water tracks, corrosion risk, or displaced gaskets. A unit that continues to operate immediately after spraying may still contain hidden moisture that causes later insulation failure or optical contamination.
Invite third-party inspection when project risk is high
Third-party inspection is valuable for large orders, new suppliers, private-label programs, public installations, and shipments with strict delivery penalties. The inspector should receive the approved specification and inspection checklist in advance, not merely a general product brochure. The final report should identify sampled serial numbers, observed defects, test equipment, nonconformities, corrective actions, photographs, and release status.
Buyers should distinguish between a pre-shipment inspection and a laboratory certification. An inspection confirms the condition of sampled goods at a defined time; it does not replace design validation, regulatory compliance, or long-duration field testing. The strongest procurement process uses all three layers: product qualification before mass production, process control during manufacturing, and shipment verification before payment or loading.
Why Colorful Light Supports a More Controlled Procurement Process
Manufacturing and quality-control capability
Colorful Light is a professional LED stage lighting manufacturer located in Room 1401, Building 4, Taoyuan Valley Science And Technology Innovation Park, No. 17 Sanshan Avenue, Guicheng Street, Foshan, Guangdong, China. The company specializes in the production, marketing, and research and development of LED stage lights, with a focused product strategy centered on LED technology and low-consumption performance.
Our manufacturing process begins with material selection and rechecking before production. Two to three quality-control members are assigned to each production line to conduct inspections throughout assembly rather than relying only on a final carton check. This layered approach helps identify wiring errors, component variation, cosmetic defects, assembly inconsistencies, and functional problems earlier in the process. Buyers can also request third-party inspections, an important option for distributors, rental companies, venue operators, and international project owners that require independent release evidence.
Product coverage for professional applications
Our portfolio includes strobe lights and blinder lights for concerts, broadcast environments, touring shows, and high-impact effects; moving head lights, LED moving heads, and wash lights for automated beam placement and color coverage; par can lights for event and stage illumination; city color lights for large-area outdoor effects; retro lights for decorative entertainment spaces; follow spot lights for performer tracking; and laser lights for specialized visual production. Product selection can therefore be coordinated across a project instead of being fragmented among multiple suppliers with different control, spare-part, and warranty practices.
For weather-exposed installations, buyers should still audit the exact model and configuration. Our technical discussions can address enclosure construction, LED power, optics, control requirements, mounting conditions, thermal expectations, packaging, and inspection scope before shipment. This helps align a fixture’s actual use case with the project’s environmental and performance requirements rather than treating an ingress rating as the only qualification criterion.
Compliance, warranty, and long-term value
Our products are CE and RoHS certified and are supplied with a one-year warranty. These documents should be reviewed alongside the model number, technical file, inspection records, and agreed commercial terms. Quality evidence is most valuable when it is connected to a clear after-sales process covering troubleshooting, replacement parts, software support, and communication with the purchasing organization.
Colorful Light has earned customer praise through advanced technology, stable performance, product quality, and service, while continuing to pursue total customer satisfaction. Our mission is to remain committed to further LED research and development and to provide low-consumption LED products for loyal customers. For buyers, this focus can support lower operating energy, consistent visual performance, simplified sourcing, and a more predictable total cost of ownership when the equipment is properly specified and audited before shipment.
Final Release Checklist for Buyers
Documents to approve
Before authorizing dispatch, confirm the approved specification, commercial invoice, packing list, serial-number register, test records, warranty statement, conformity documents, user manual, wiring information, spare-parts list, and inspection report. The model designation on every document should match the physical product and carton label. Any engineering change made after sample approval should be disclosed and revalidated.
Physical checks to complete
Verify enclosure seals, cable glands, connectors, fasteners, lenses, brackets, handles, safety cables, labels, displays, accessories, and spare fuses where applicable. Confirm that cartons contain the promised power cables, signal cables, clamps, manuals, protective covers, and replacement components. Photograph pallet condition and carton markings before loading, especially for export shipments exposed to multiple handling points.
Commercial release decision
Release should be based on documented conformity, not schedule pressure. Classify findings as critical, major, or minor; define corrective action and reinspection requirements; and retain the final evidence with the purchase record. This disciplined approach reduces field failures, emergency freight, installation delays, warranty claims, and reputational damage for distributors and project owners.
Frequently Asked Questions
Does an IP65 rating mean a stage light can be submerged?
No. The second digit five indicates protection against water jets under defined test conditions; it does not automatically qualify the fixture for immersion, high-pressure cleaning, or unrestricted extreme-weather exposure.
What documents should buyers request before shipment?
Buyers should request the approved product specification, bill of materials, wiring diagram, user manual, risk assessment, inspection plan, sample approval record, model-specific ingress test evidence, serial-number register, electrical and burn-in records, conformity documents, warranty statement, and packing list.
Should every fixture be tested for ingress protection?
Sampling may support visual and dimensional checks, but critical safety or ingress-related characteristics may require 100% verification or a dedicated test on representative samples, depending on product value, failure consequences, production maturity, and project scale.
What should a factory burn-in test include?
A controlled aging cycle should operate sampled units through realistic scenes, including high-output white, saturated colors, dimming transitions, strobe operation, movement patterns, and signal interruption where relevant, while monitoring restarts, flicker, error codes, thermal alarms, fan changes, and communication loss.
Can CE and RoHS documents prove that a fixture is IP65 compliant?
No. CE marking concerns applicable EU requirements and RoHS concerns restrictions on certain hazardous substances. Neither document by itself proves that a particular luminaire passed an ingress protection test; buyers need model-specific test evidence and inspection records.
Why is third-party inspection useful for stage lighting orders?
Third-party inspection provides independent evidence of the condition of sampled goods at a defined time. It is especially useful for large orders, new suppliers, private-label programs, public installations, and shipments with strict delivery or quality requirements.
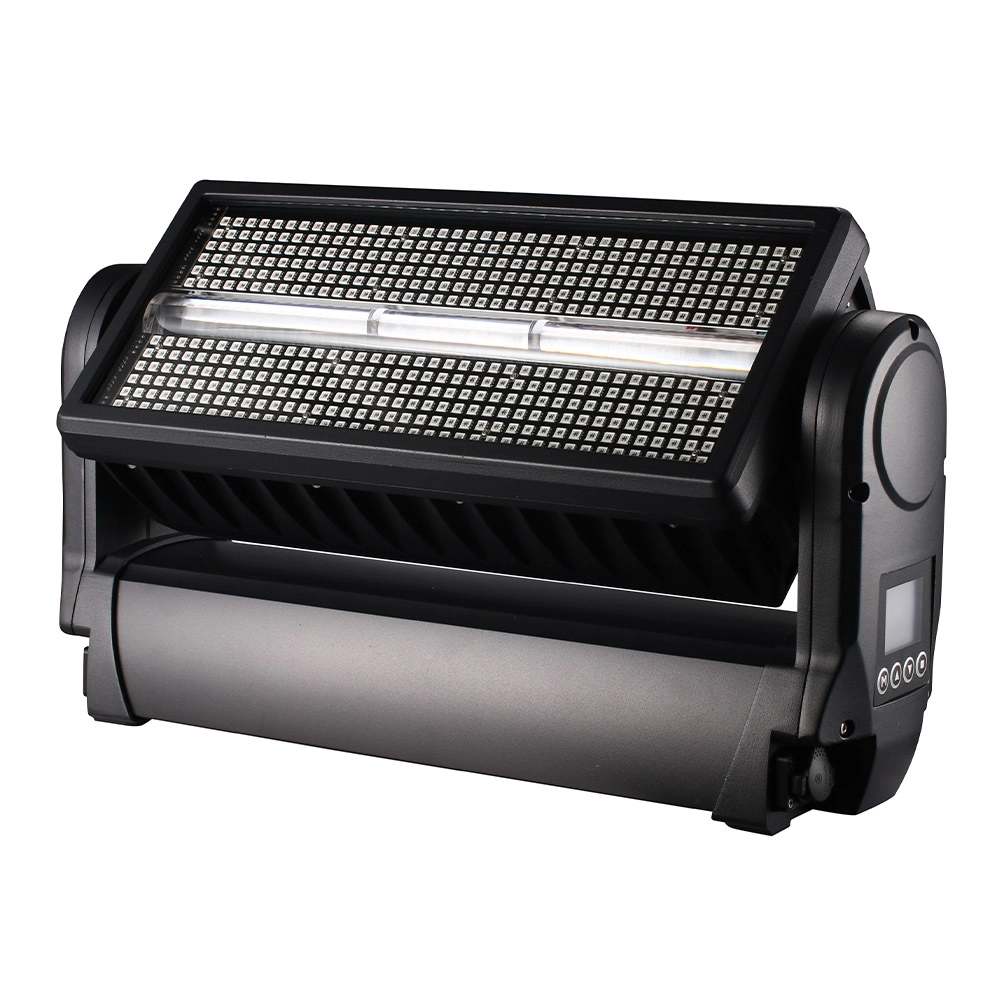
The 1000W Outdoor LED strobe moving light is a high-power outdoor strobe moving light equipped with a 1000W high-brightness LED light source. It supports strobe frequency adjustment and precise head-shaking positioning, and has an IP65 protection rating, which can withstand outdoor rain, snow, and dust.
It is compatible with DMX512 control, and has a powerful and stunning light effect, making it suitable for creating dynamic light and shadow effects in outdoor music festivals, large-scale cultural and tourism night tours, open-air celebrations, and other scenarios.(jdc1 version optional)

24*20W RGBW IP65 waterproof LED wash floodlight. Features uniform RGBW four-color mixing, 6 segement.W-DMX(optional).IP65 protection to withstand complex outdoor weather conditions, flexible light control, and suitability for architectural lighting, cultural and tourism landscapes, and other applications.( support sgm P6 channel)

The Epic Strobe 600w waterproof matrix strobe light is a high-power waterproof strobe light equipped with a 600W high-brightness LED light source. The strobe frequency is adjustable and the brightness is strong.
It supports seamless splicing expansion of multiple panels, has a high level of waterproof performance, is compatible with DMX512 control, and is flexible in installation. It is suitable for creating stunning light and shadow effects in outdoor large-scale performances, cultural and tourism light shows, building facade lighting and other scenarios.

The Waterproof 2x475W LED Blinder matrix Light features a powerful 600W LED light source, delivering strong luminous efficiency and outstanding brightness to instantly illuminate the entire area and create a stunning visual impact.
Its IP65 high-level waterproof and dustproof design, along with its robust and reliable sealed structure, withstands heavy rain and strong dust, making it suitable for stable operation in all weather conditions in outdoor settings.
Colorful Light is a professional LED stage lighting manufacturer that provides dynamic and reliable lighting solutions to customers worldwide.
© 2026 Colorful Light. All Rights Reserved.

Facebook
Instagram
LinkedIn
YouTube
Tik Tok